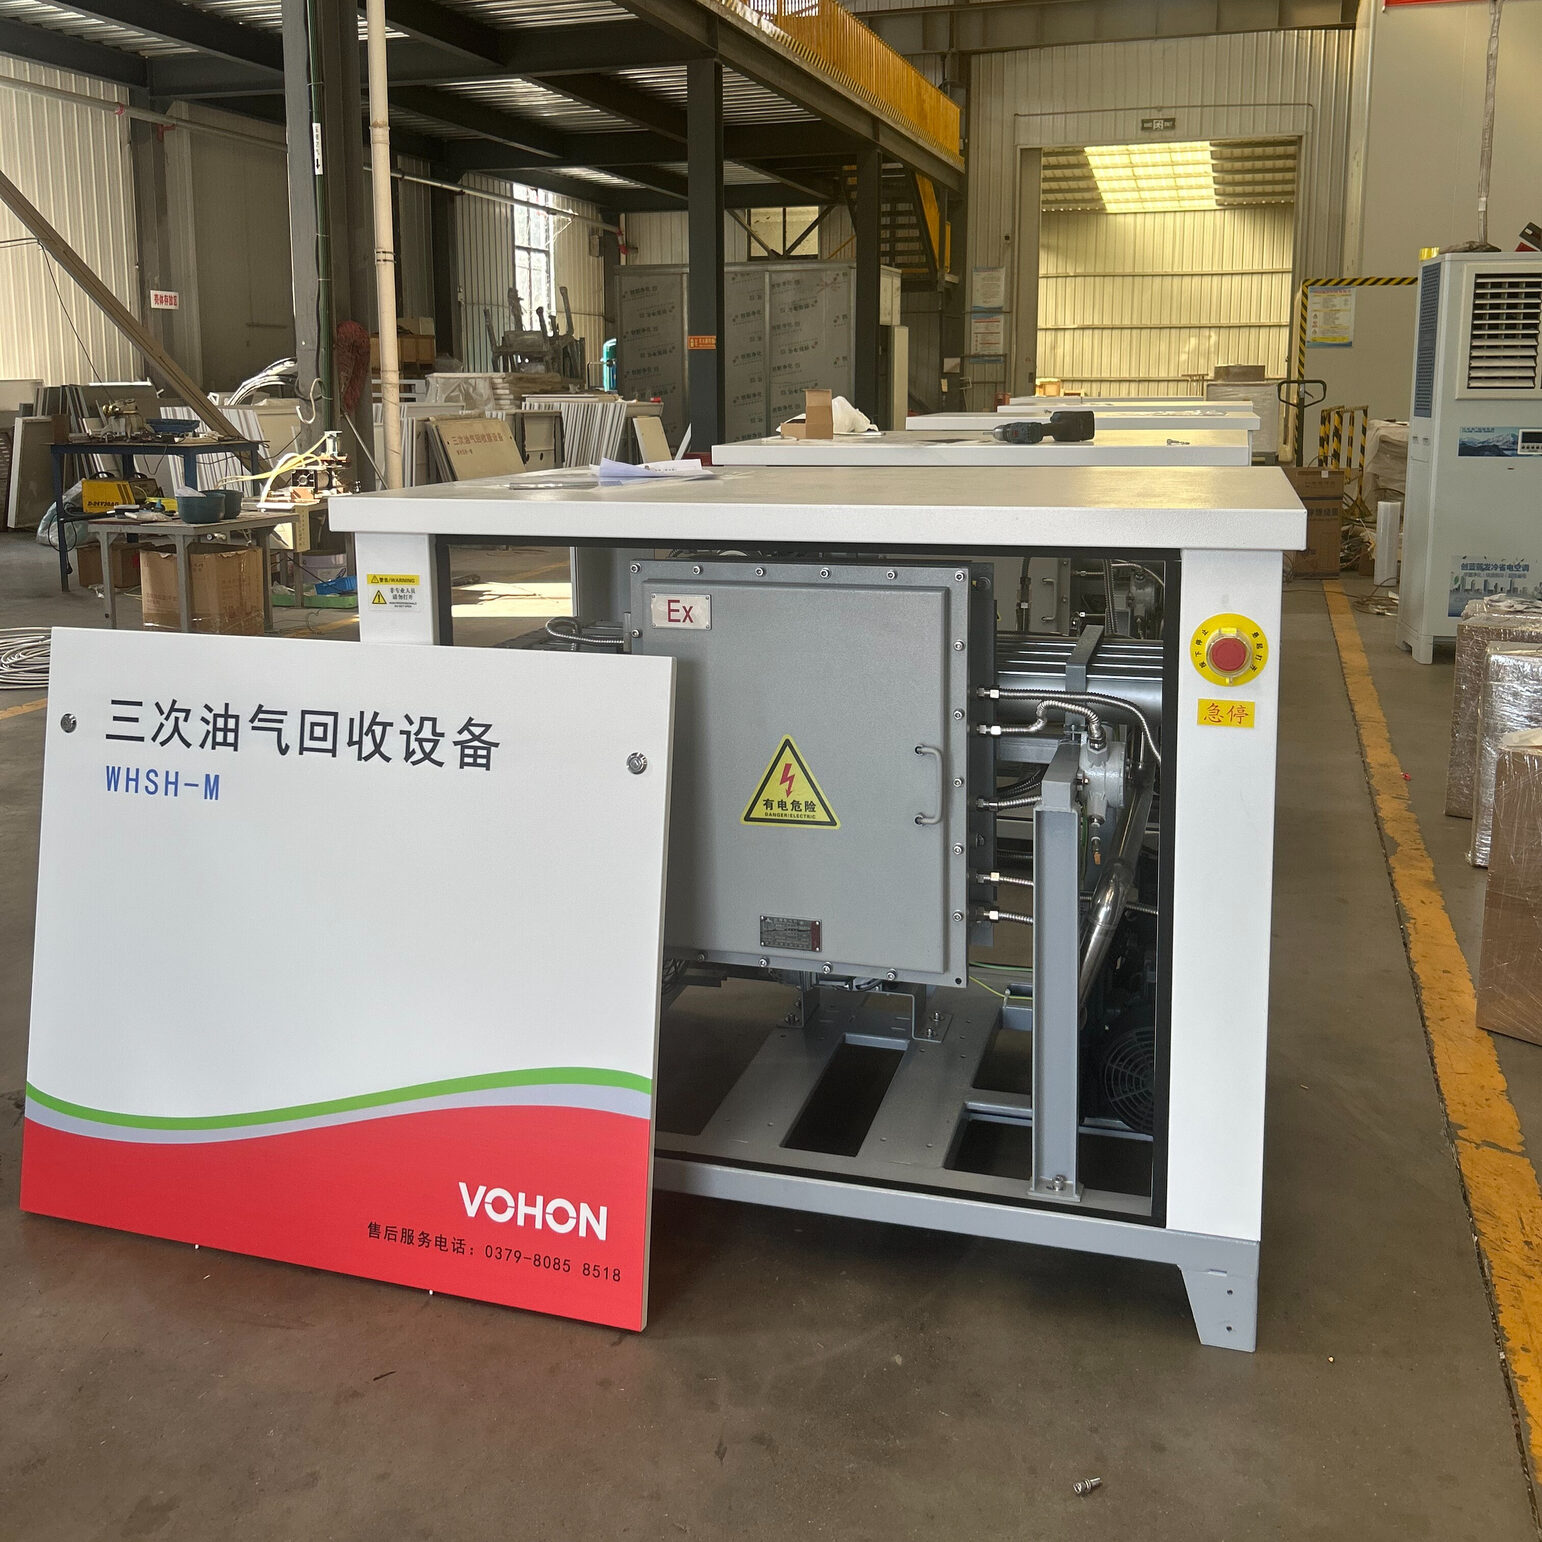
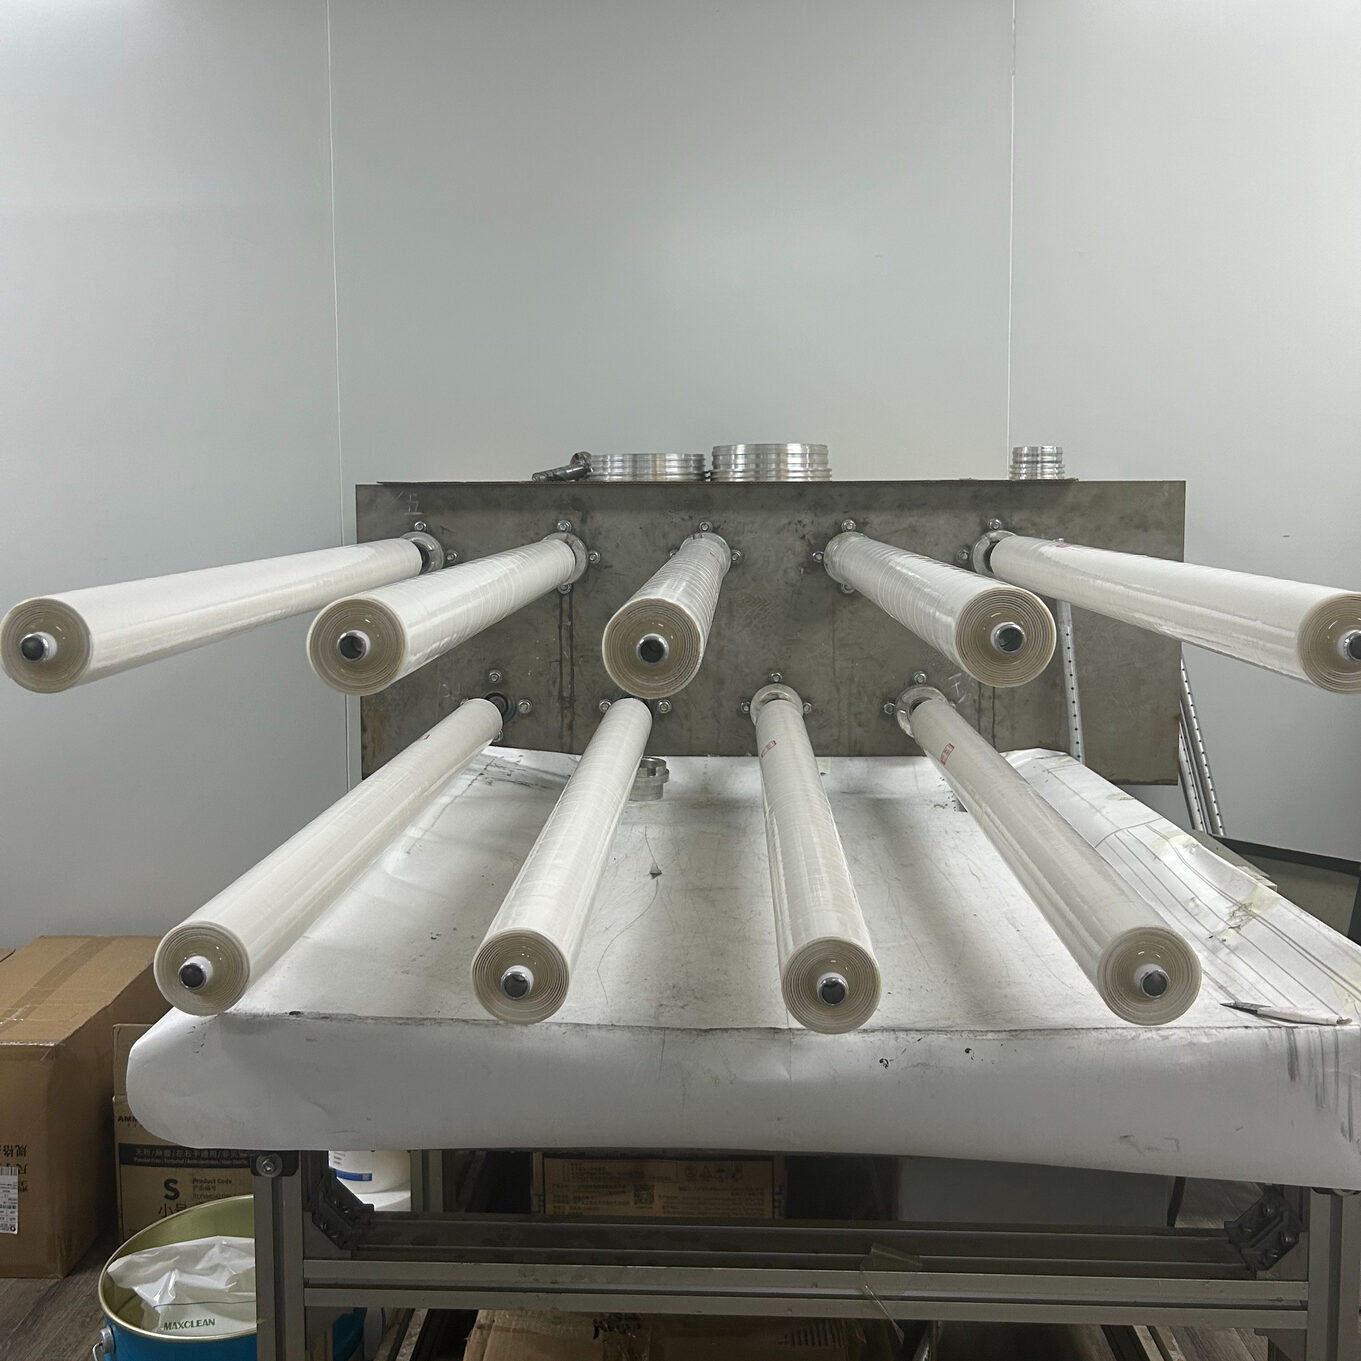
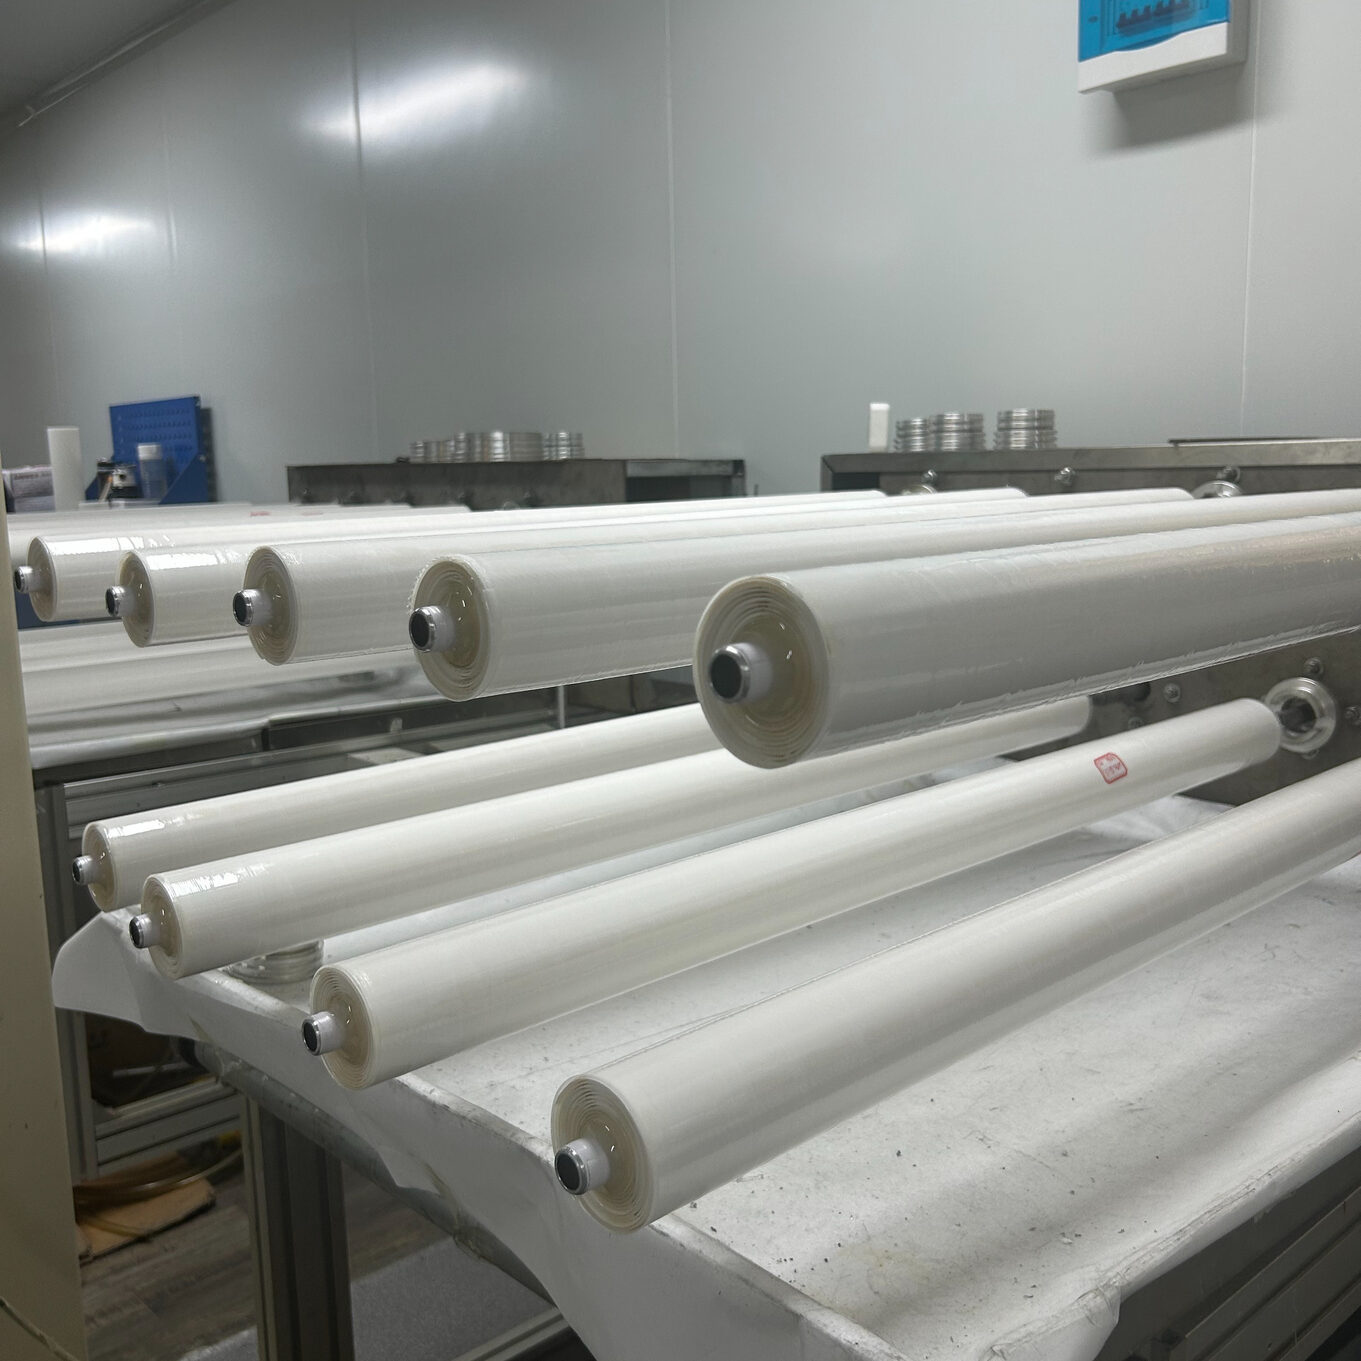
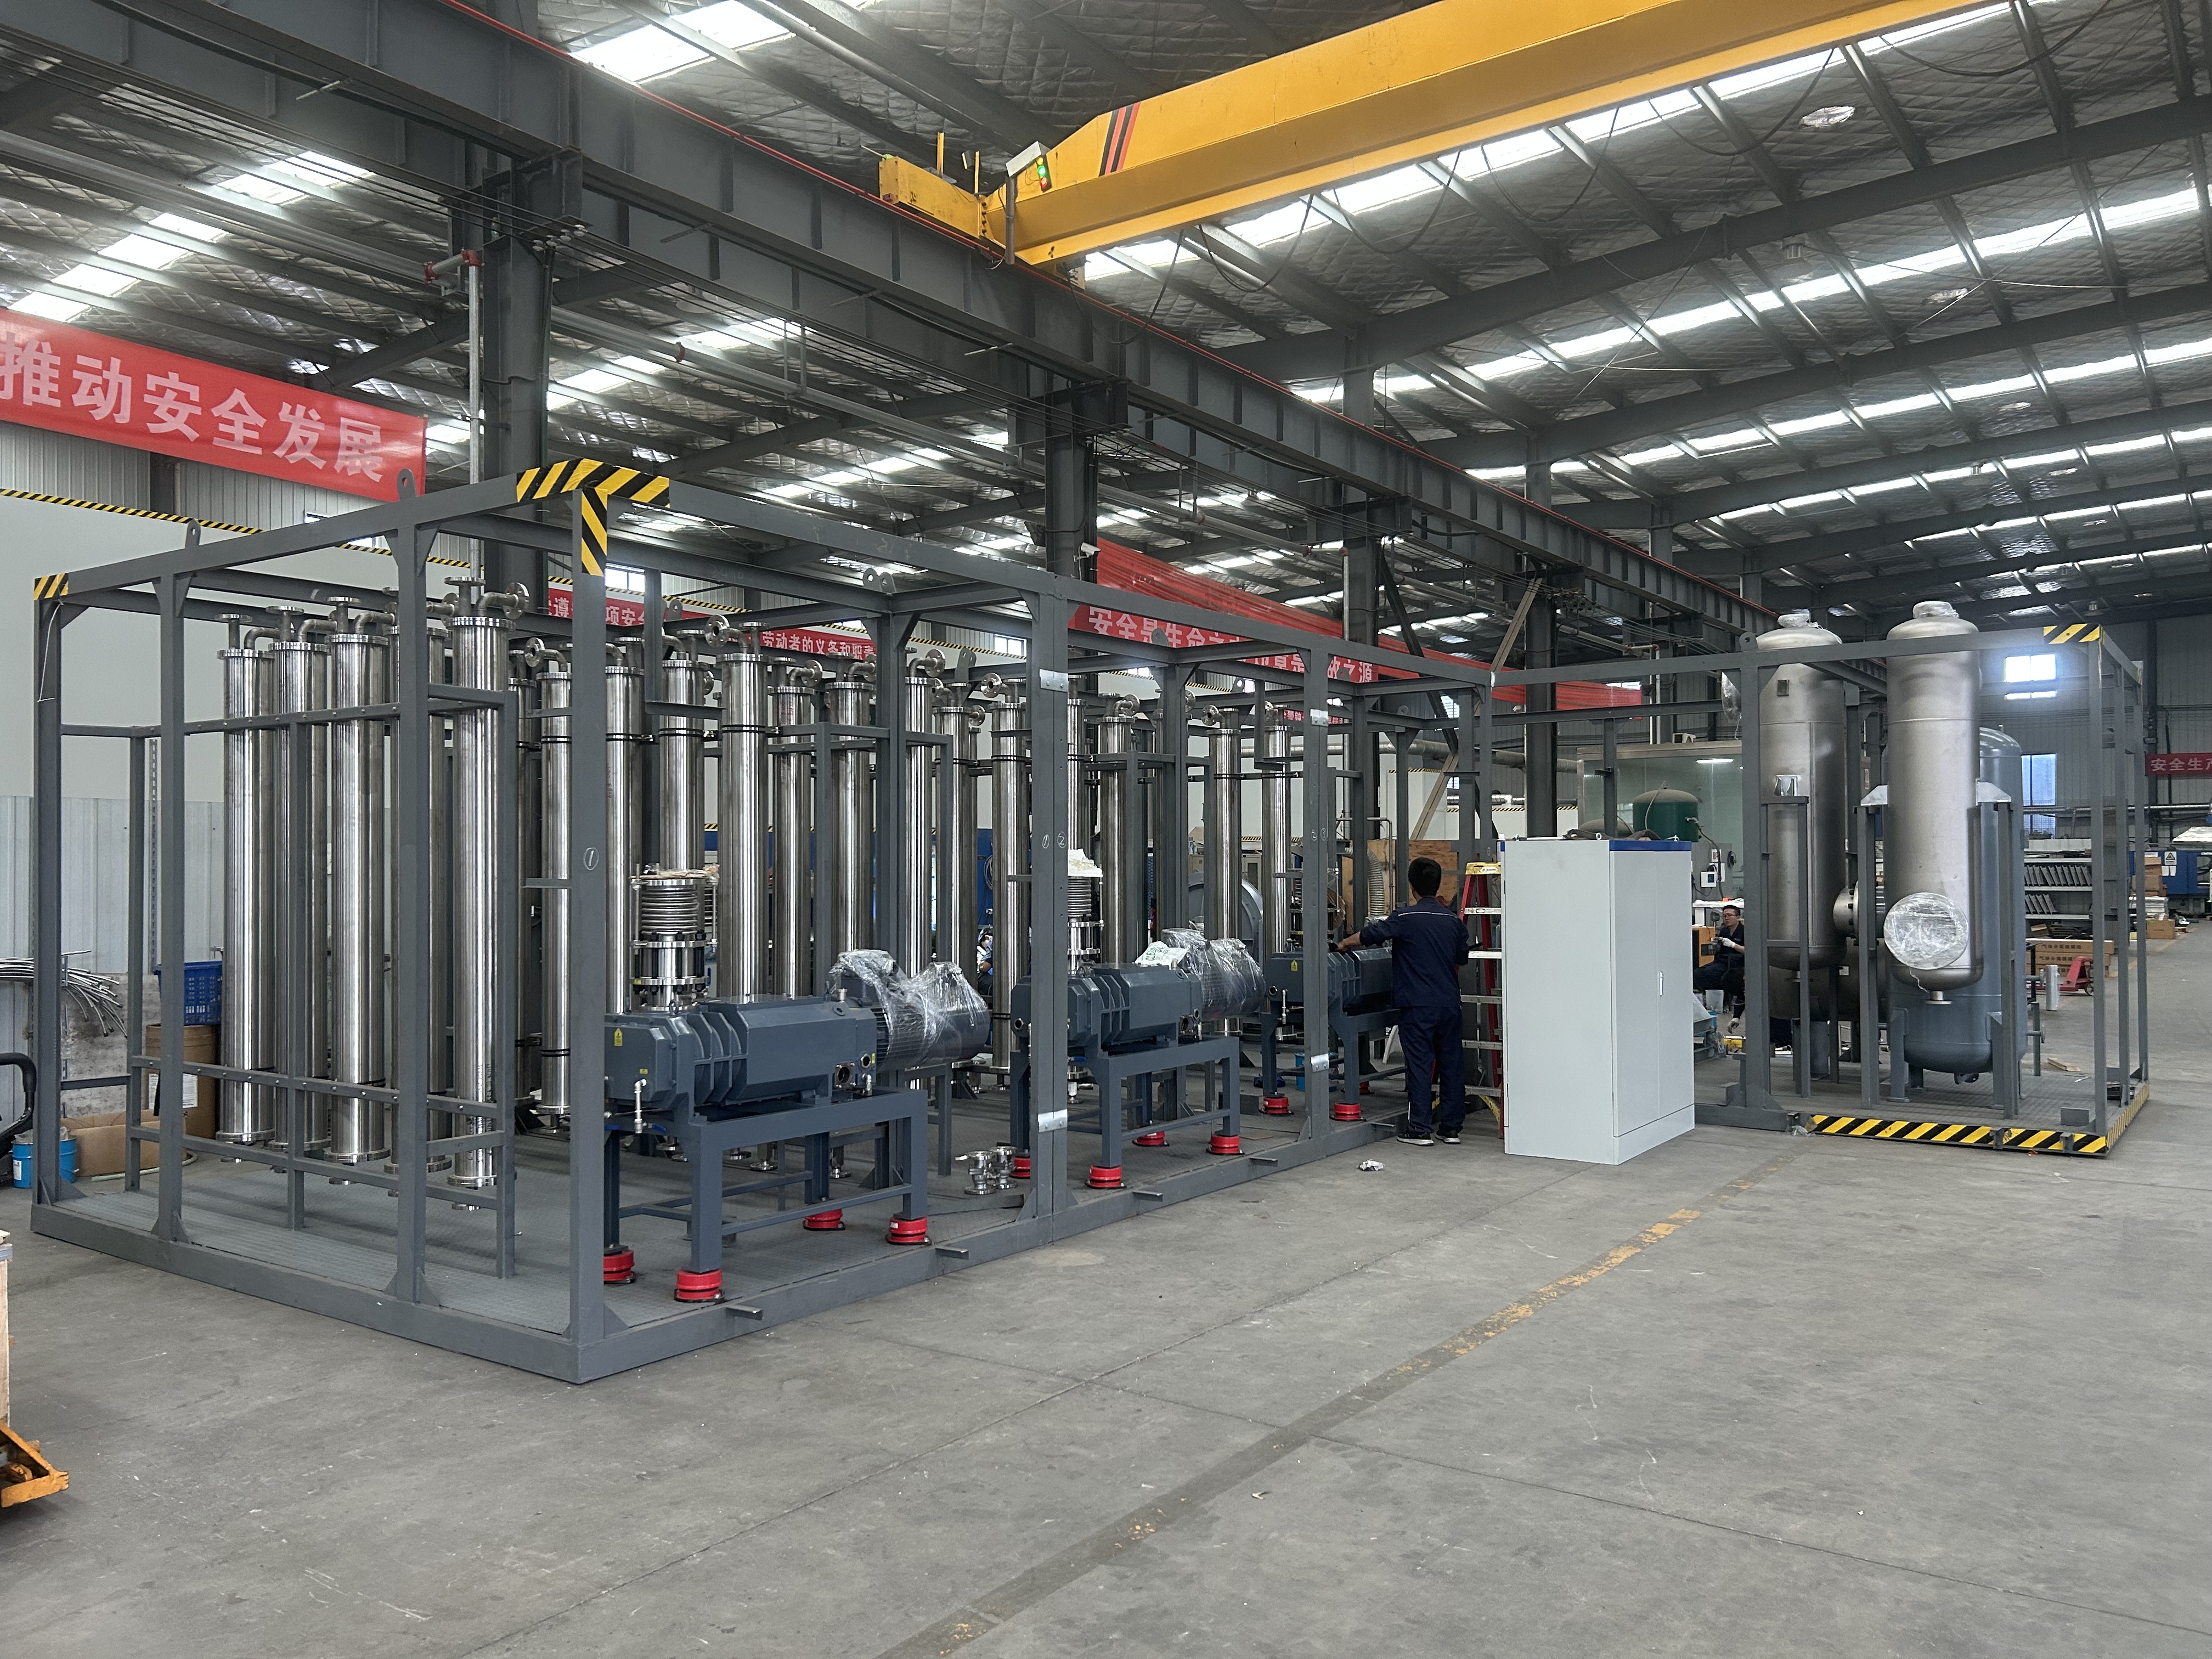
The device is dedicated to the recovery and treatment of volatile gases from low boiling point organic solvents such as petroleum ether, with a processing capacity of 800m ³/h. It adopts a combination process of "vacuum negative pressure collection+compression condensation+membrane separation". After the volatile gas is collected through a closed pipeline, it is first compressed and condensed, and most of the petroleum ether is liquefied and recovered; The uncondensed low concentration exhaust gas enters the membrane separation unit, and the organic gas is preferentially enriched and refluxed through the membrane for cascade treatment, resulting in clean air emissions meeting standards. The recovery rate can reach over 95%, and the emission concentration is far below the national emission limit. There is no solid waste, no waste liquid, and no secondary pollution. Explosion proof design of the device, PLC fully automatic control, integrated installation, small footprint, low energy consumption, long lifespan of membrane components, simple operation and maintenance, suitable for solvent recovery and exhaust gas treatment in petroleum ether use sites in industries such as pharmaceuticals, chemicals, and coatings.
Mr. Li 13526990215

Hotline